Computer vision versus manual inspection: compare accuracy, cost, speed, traceability, and deployment needs for factories, warehouses, and logistics teams
A rejected carton at the end of a line is rarely just one rejected carton. It can mean rework, a late shipment, a disputed supplier claim, or an audit question with no clear answer. The decision around computer vision versus manual inspection is therefore not simply about replacing people with cameras. It is about deciding where judgment belongs, where evidence is required, and how consistently critical checks must happen across every shift and site.
Manual inspection remains valuable in industrial operations. Experienced operators recognize subtle defects, understand context, and can respond when product, packaging, or conditions change unexpectedly. But when inspection volume rises, tolerance windows narrow, or proof of execution becomes necessary, human-only controls become difficult to scale.
Computer Vision Versus Manual Inspection: The Core Difference
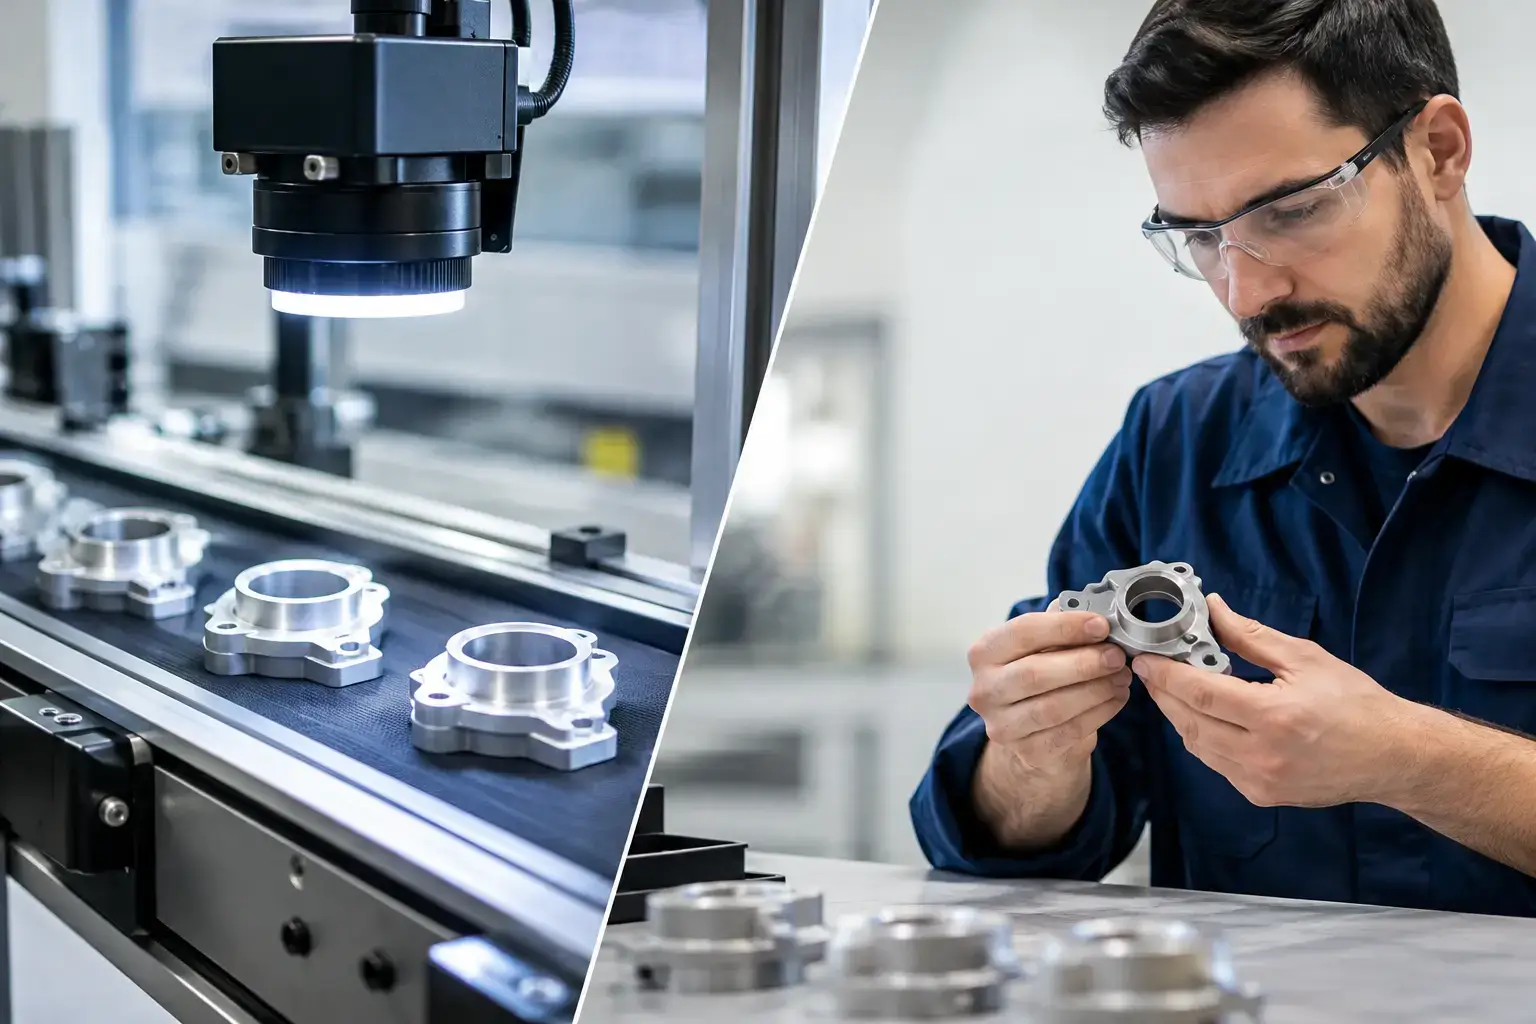
Manual inspection relies on an operator to observe, interpret, decide, and record an outcome. The quality of the result depends on training, attention, lighting, workload, fatigue, and how clearly the inspection standard has been defined. It works best where exceptions are varied, volumes are manageable, and the cost of a missed defect is low enough to accept some inconsistency.
Computer vision uses cameras and software models to detect defined visual conditions. Depending on the use case, the system can verify label presence, check seal integrity, count items, detect PPE compliance, identify unauthorized area access, read codes, monitor congestion, or flag product anomalies. It applies the same rule repeatedly and can retain time-stamped evidence of every event.
That consistency is the major operational difference. A trained inspector may notice a problem that was never anticipated during system design. A vision system may inspect thousands of similar units without losing concentration. Neither approach is universally better. The correct choice depends on process stability, inspection criticality, cost of failure, and the organization’s readiness to act on the data generated.
Where Manual Inspection Still Makes Business Sense
A manual process is not automatically a weak process. For low-volume work, highly customized products, new product introduction, or defects that require tactile assessment, human inspection can be the most commercially sensible control.
Consider a fabrication workshop producing short-run assemblies. Each unit may differ in finish, component configuration, and customer requirements. An experienced quality technician can interpret drawings, assess fitment, and decide whether a visual variation is acceptable in a way that a narrowly trained model may not. The same applies to complex maintenance inspections where sound, vibration, smell, or physical movement affect the diagnosis.
Manual checks are also useful as an escalation layer. A vision system can identify a damaged pallet, unreadable label, missing cap, or line-side safety breach. A supervisor or quality operator can then determine the disposition, root cause, and corrective action. This creates a practical division of labor: machines perform continuous observation, while people handle exceptions and decisions with broader operational consequences.
The weakness appears when the manual process is asked to provide high-frequency, audit-grade verification without adequate controls. Paper checklists completed after the fact, visual checks recorded only as a tick mark, and inspections that vary by shift provide limited defensibility when a customer complaint or regulator asks what happened.
Where Computer Vision Creates Measurable Value
Computer vision produces the strongest return when a visual check is repetitive, frequent, and tied to a measurable business risk. The value does not come from having AI in a camera. It comes from reducing defects, preventing losses, improving compliance, and providing usable evidence to the teams responsible for execution.
In manufacturing, vision can inspect products at speed for missing components, incorrect orientation, packaging defects, label mismatches, or incomplete assembly. It can also monitor process conditions such as work-in-progress accumulation, machine idle time, or whether required procedures are being followed at a station. When connected to production and quality workflows, an alert can trigger containment before a batch moves further downstream.
In warehousing and logistics, use cases include dock-door verification, pallet counting, vehicle turnaround monitoring, damaged-goods detection, zone access control, and proof that loading activities occurred in the required sequence. Cold-chain teams can combine CCTV-based verification with telemetry records to show not only that a temperature excursion occurred, but also what operational activity was happening around the event.
Safety and compliance are equally relevant. A camera-based system can flag missing helmets or high-visibility vests in defined zones, detect intrusion into restricted areas, and document whether a process was performed. The goal should not be surveillance for its own sake. It should be clear operational control, applied transparently and governed with appropriate policies.
Accuracy Is Not a Simple Percentage
Buyers often ask whether computer vision is more accurate than a person. The useful answer is: accurate at what, under which conditions, and with what response process?
A vision model may achieve high detection rates in a controlled scene with stable camera angles, adequate lighting, clear product presentation, and a well-defined defect class. Its performance can drop if packaging changes, reflective surfaces create glare, cameras are moved, or a new product variant enters the line without retraining. A system that performs well in a pilot can underperform after go-live if site conditions are not managed.
Manual inspection has comparable dependencies. A skilled operator can achieve excellent results when inspecting a limited number of units under appropriate conditions. Accuracy falls when they are simultaneously handling production pressure, documentation, shift handovers, and frequent interruptions.
For this reason, serious deployments measure false positives and false negatives, not only a headline accuracy rate. A false positive creates unnecessary intervention. A false negative allows a defect, safety issue, or compliance failure to pass unnoticed. The acceptable balance differs by process. A pharmaceutical packaging line, a high-value electronics operation, and a warehouse dock have different risk thresholds.
Cost: Look Beyond Headcount
Manual inspection can look less expensive because labor is already assigned to the line or warehouse. Yet the full cost includes training, supervision, inconsistent documentation, reinspection, missed defects, customer returns, downtime, and the time spent investigating incidents without evidence.
Computer vision requires upfront work. Cameras must be positioned correctly, network and storage requirements addressed, use cases defined, models configured, and workflows connected to the right teams. There are also ongoing costs for maintenance, model refinement, hardware replacement, and operational support.
The commercial case is strongest when the system addresses a known loss point. Examples include repeated mislabeling, frequent loading disputes, high rework rates, safety nonconformance, or a quality check that requires dedicated labor around the clock. A deployment should start with a baseline: current defect rate, labor time, incident cost, inspection volume, and response time. Without that baseline, ROI becomes a promise rather than a measurable operating result.
The Best Model Is Often Hybrid
Most industrial organizations should not frame this as a winner-takes-all choice. A hybrid model is frequently more reliable and easier to adopt.
Computer vision can perform the first-pass check continuously, record evidence, and create an exception case when confidence falls below an agreed threshold. Human operators then review exceptions, validate edge cases, and feed confirmed outcomes back into process improvement. This reduces repetitive checking while retaining experienced judgment where it matters.
For example, a warehouse can use vision to verify that pallets entering a staging area carry the expected labels and are placed in the correct zone. If the label is obscured or the pallet configuration is unusual, the system can route the exception to a supervisor. The supervisor does not need to inspect every movement, only the ones that need a decision.
This model also supports change management. Teams are more likely to trust a system that helps them focus on real exceptions than one positioned as a black-box replacement for operational expertise.
Deployment Requirements That Determine Success
The technology selection matters, but execution matters more. Before deploying vision, operations and IT leaders should define the inspection event, pass-fail criteria, required evidence, response owner, and escalation path. If an alert has no owner or a defect has no defined disposition, the camera becomes another dashboard nobody uses.
Site readiness is equally important. Camera placement, lighting, product variation, connectivity, retention policies, cybersecurity, and privacy requirements need attention before scale-up. Integration should be planned from the beginning. Vision events often need to connect with ERP transactions, warehouse tasks, maintenance tickets, quality nonconformance workflows, or management dashboards.
A platform such as SnapAI Vision can make the operational layer more usable when vision detections feed configurable workflows, role-based alerts, audit trails, and enterprise systems rather than remaining isolated video events. The objective is not more footage. It is faster, documented action.
Start with one process where the business cost is visible and the visual condition is clearly defined. Prove the detection performance, response discipline, and financial impact in live operations. Then expand to the next bottleneck with a deployment model your team can use on Monday.
KEEP READING
Want the version that applies to your operation?
Articles only go so far. Book a no-obligation session and we'll walk your process end to end.
Book a demo →