Learn how to manage production wastage with traceable data, root-cause control, and practical workflows that protect quality, yield, and margin daily.
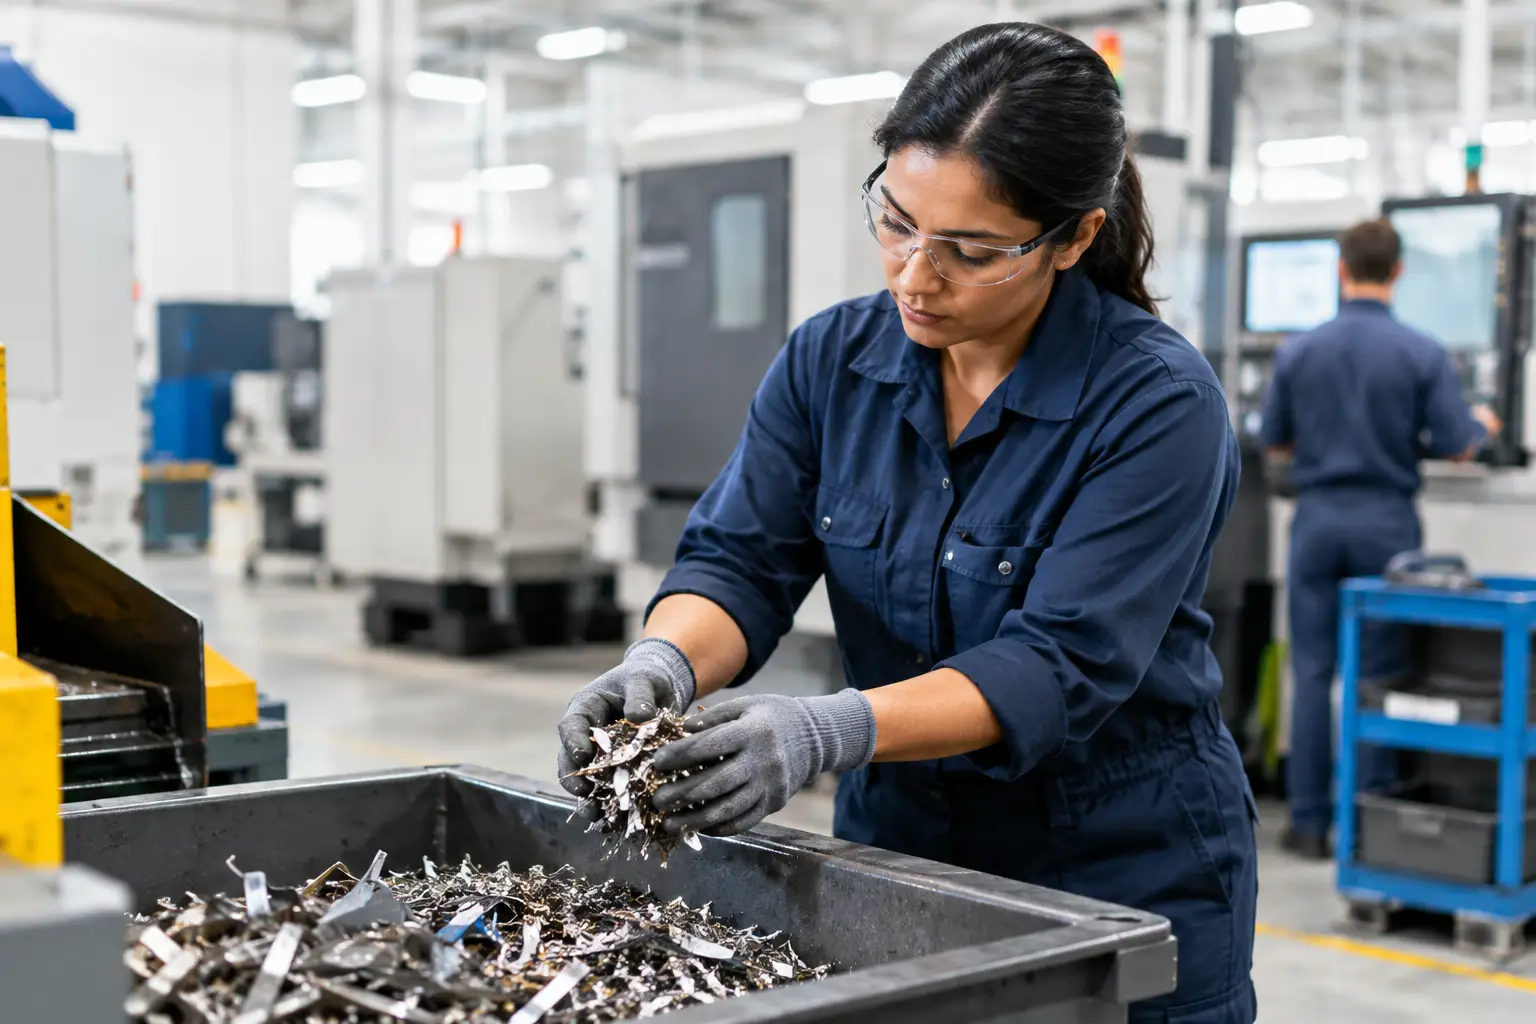
A rejected batch is rarely just a rejected batch. It can mean lost raw material, unplanned labor, missed shipment windows, rework queues, inventory discrepancies, and difficult questions during the next quality review. Learning how to manage production wastage starts by treating waste as an operational signal, not simply an unavoidable cost of production.
The objective is not to drive every waste figure to zero. Some loss is inherent to cutting, changeovers, sampling, cleaning, startup runs, and quality control. The operational requirement is to distinguish expected loss from preventable loss, record it consistently, and act on it before it becomes a recurring margin leak.
Start With a Wastage Definition the Floor Can Use
Many factories have a wastage percentage in a monthly report but no common definition at the point where loss occurs. Operators may classify an issue as scrap, while quality labels it as rejected material and finance records it as a variance. That fragmentation makes the total look precise while hiding the cause.
Establish a practical wastage taxonomy that matches the production process. Typical categories include process scrap, quality rejection, rework, damaged raw material, expired material, setup loss, packaging loss, and unexplained variance. Each category should have a clear owner, a reason code, and a defined disposition: reuse, rework, return, quarantine, disposal, or sale as by-product.
This is not administrative overhead. A reason code such as “quality issue” does not support corrective action. “Seal temperature below control limit during Line 3 startup” does. The level of detail should be sufficient to identify a repeatable condition without making floor capture so slow that people bypass it.
Measure Wastage Where It Happens
End-of-shift or end-of-month reporting is too late for operational control. By then, the material is gone, the conditions have changed, and teams are left reconstructing events from memory.
Capture wastage at the machine, line, work order, batch, or production step where it occurs. The record should tie together the material lot, product or SKU, quantity, unit of measure, shift, operator or team, machine, reason code, and disposition. Where relevant, include process parameters such as temperature, speed, pressure, humidity, weight, or downtime event.
The best capture method depends on the environment. A high-volume line may require automated counters and IoT telemetry. A discrete assembly operation may need a tablet workflow with barcode scanning. For visual defects, camera-based inspection can identify and classify issues before defective output moves further downstream. The principle is consistent: capture facts at the source, with as little manual re-entry as possible.
A digital record also prevents a common control failure: scrap being physically removed while inventory and production records remain unchanged. When the shop floor, warehouse, quality team, and finance function work from different numbers, no one can confidently calculate true yield or product cost.
Use Yield, Not Just Scrap Cost, to Manage Production Wastage
Scrap cost is essential, but it is a lagging financial result. Yield reveals whether the process is producing the expected output from the input consumed.
For a production order, calculate actual yield against the standard or planned yield. Then segment the result by product family, line, machine, shift, supplier lot, and reason code. A plant-wide average can conceal a serious problem in one SKU or one operating window.
Track a small set of measures that decision-makers can use:
- Material yield: acceptable output divided by material input.
- Scrap and rework rate: lost or recoverable quantity as a percentage of total production.
- First-pass yield: output that meets specification without rework.
- Cost of poor quality: scrap, rework labor, disposal, downtime, replacement material, and related freight.
- Unexplained variance: the gap between expected and recorded material consumption.
The trade-off matters. A lower scrap rate is not automatically an improvement if teams are reclassifying defects as rework and creating a larger capacity bottleneck. Likewise, reducing inspection may improve reported throughput while increasing customer returns. The right target protects quality, delivery performance, and gross margin together.
Find the Cause Before You Automate the Fix
Once wastage is visible by source, investigate patterns rather than isolated incidents. Start with the highest-cost or highest-frequency category, then review the conditions around it. Is the loss concentrated after changeovers? Does it follow a particular supplier lot? Is it associated with a machine alarm, a maintenance interval, a shift handover, or a specific formulation revision?
A structured root-cause review should connect four areas: material condition, equipment performance, method or work instruction, and people or training. It should also consider measurement. If scales are not calibrated, scanners are bypassed, or units of measure are inconsistent, the reported waste may be inaccurate before the investigation even starts.
Use a simple containment-to-correction workflow. First, prevent additional loss by holding the affected material, slowing the line, adjusting a parameter, or increasing inspection. Next, verify the cause with production, maintenance, quality, and supply chain data. Then assign a corrective action with an owner, due date, validation method, and audit trail.
This is where many improvement programs fail. A meeting may identify the issue, but the action is stored in email or a spreadsheet and is never verified on the floor. Closed-loop workflow matters because it makes corrective action part of daily execution, not a report recommendation.
Build Controls Into Production Workflows
The strongest wastage controls happen before material becomes scrap. Standardized digital workflows can require the checks that operators and supervisors need at the moment of execution.
For example, a line-start checklist can verify the correct material lot, recipe version, machine settings, cleaning status, and first-off inspection before full production begins. During the run, sensor readings can trigger alerts when a process approaches its control limit. At shift handover, an operator can record active quality concerns, remaining material, and machine conditions instead of relying on verbal updates.
For perishable, regulated, or lot-controlled materials, integrate inventory rules with production consumption. FEFO handling, lot traceability, quarantine controls, and expiry alerts reduce the chance that unsuitable material reaches the line. For multi-site operations, the same workflow structure creates comparable data without forcing every facility into an identical physical process.
Snapdec deployments typically connect these floor workflows with AI vision, telemetry, warehouse records, and ERP transactions so teams can trace a loss from material receipt through production, disposition, and financial impact. The practical value is not another dashboard. It is an audit-grade operational record that allows a manager to see what happened, who acted, and whether the corrective action worked.
Make Accountability Fast and Specific
Production wastage is cross-functional, but it should not become ownerless. Production owns execution against standard work. Quality owns specification and disposition controls. Maintenance owns equipment reliability. Warehouse and procurement own material handling and supplier performance. Finance validates valuation and cost impact. Leadership removes obstacles and prioritizes improvement work.
A daily review should focus on exceptions, not a long presentation of every metric. Review yesterday’s material variance, major scrap events, repeat reason codes, open corrective actions, and any risk to customer orders. The discussion should end with named actions, not general commitments to “monitor the situation.”
Weekly reviews can look for trends across shifts, sites, suppliers, and product lines. Monthly reviews should connect operational improvements to financial results, including whether reduced waste also lowered write-offs, overtime, expedited freight, or customer claims.
Scale What Works, But Keep the Process Honest
A pilot on one line is useful only when the controls can operate under real production pressure. Test the workflow during changeovers, network interruptions, urgent orders, operator absences, and maintenance events. If people need three extra screens to log a defect, the data quality will decay as volume increases.
Start with one material-intensive process or one recurring loss pattern. Establish a baseline, digitize the capture and response workflow, and prove that the intervention reduces a specific source of loss. Then replicate the model with configurable reason codes, approval rules, and integrations for each site.
The most effective wastage programs make loss visible while there is still time to respond. When every kilogram, component, or unit has a traceable story, managers can move from explaining margin erosion after the fact to preventing it on the next shift.
KEEP READING
Want the version that applies to your operation?
Articles only go so far. Book a no-obligation session and we'll walk your process end to end.
Book a demo →