Cold storage compliance requires more than temperature logs. Build traceability, alerts, corrective action, and audit-ready records across every shift.
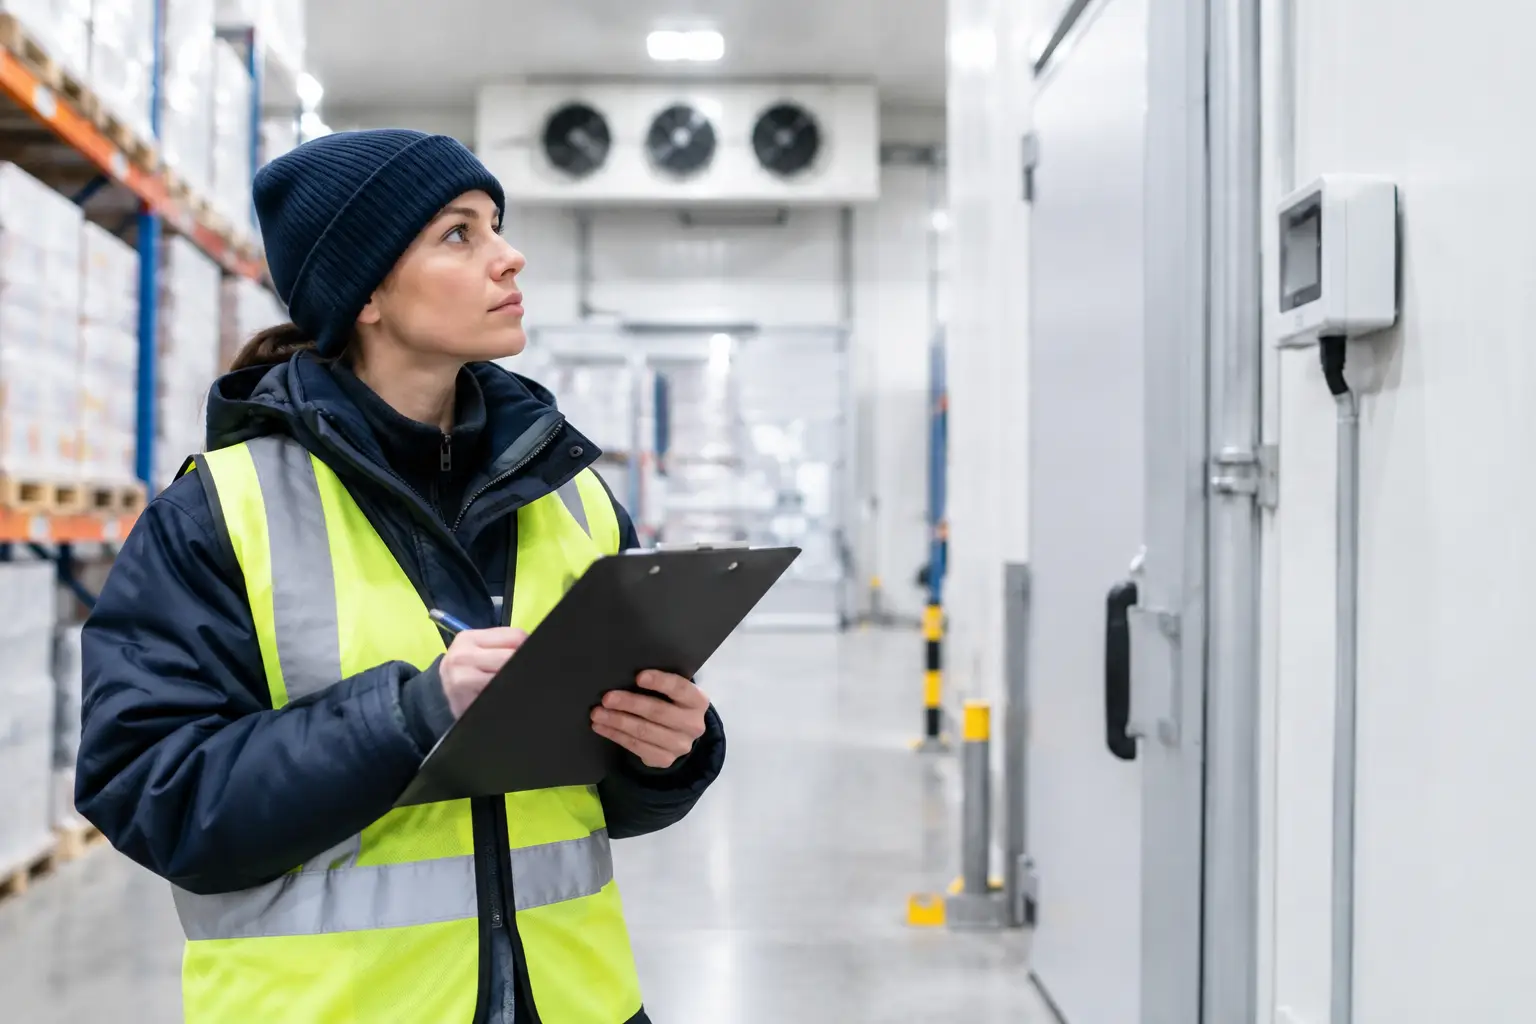
A refrigerated warehouse can appear under control right up until an auditor asks a simple question: what happened to this pallet during the two hours when Dock 4 was open, the temperature alarm sounded, and the supervisor was off shift? Cold storage compliance is not proven by a walk-in freezer, a clipboard, or a monthly calibration certificate. It is proven by complete, time-stamped evidence that connects conditions, inventory, people, decisions, and corrective action.
For food, pharmaceutical, life sciences, and temperature-sensitive distribution operations, the practical challenge is making that evidence available without slowing down receiving, putaway, picking, dispatch, or quality release. The strongest compliance programs treat temperature control as an operating system, not a recordkeeping exercise.
Cold Storage Compliance Starts With Controlled Workflows
Regulatory requirements differ by product, market, customer contract, and storage profile. A frozen food operator may be working against FDA food safety expectations, HACCP plans, customer standards, and local health requirements. A pharmaceutical distributor may need to meet far stricter requirements for product handling, batch traceability, validation, and electronic records. The control model must match the risk.
What does not change is the need to define the workflow before digitizing it. Teams need clear answers to operational questions: What is the acceptable temperature range for each product class? How long can product remain on a receiving dock? Who can release quarantined inventory? What happens when a sensor goes offline? Which event requires a quality review rather than an automatic exception closure?
A documented standard operating procedure is the starting point. But procedure alone does not control execution on a busy shift. The warehouse system, IoT monitoring platform, quality workflow, and physical process must enforce the same rules. If warehouse staff can put a chilled product into an ambient location because the system does not block it, the written policy has already failed.
Build controls around the product journey
Every product movement creates a possible compliance point. Receiving should capture supplier, lot or batch, expiry date where applicable, product condition, inbound temperature, inspection result, and the assigned storage zone. Putaway should verify that the destination supports the required range. Picking should apply FIFO or FEFO rules according to product and customer requirements. Dispatch should maintain chain-of-custody records through loading and handover.
The operational trade-off is straightforward. Too few controls create audit exposure and product loss. Too many manual checks create workarounds, delays, and incomplete records. The right design automates routine validation and reserves human attention for exceptions that need judgment.
Temperature Data Must Be Trusted, Not Just Collected
Many facilities have temperature sensors but cannot demonstrate that the data is reliable, complete, and acted upon. A dashboard with green and red indicators is useful for operations, but compliance requires more: sensor identity, placement, calibration status, reading frequency, retained history, alarm thresholds, user actions, and investigation records.
Sensor placement matters. Air temperature near an evaporator is not necessarily representative of product temperature at the back of a high-density rack. Door openings, loading activity, defrost cycles, airflow restrictions, and poorly sealed areas can create local variation. Mapping the room and validating sensor positions should be part of the facility's control plan, particularly after layout changes or major equipment work.
Alarms also need escalation logic. An alert sent to one employee's phone is not a compliant response process. A meaningful workflow records the alarm, identifies the responsible role, requires acknowledgment, triggers escalation if no action occurs within the defined window, and captures the corrective action taken. If a temperature excursion affects inventory, the system should place relevant stock on hold until quality or an authorized manager completes the disposition decision.
This is where connected operations deliver practical value. SnapIOT can provide telemetry visibility, while workflow automation can route incidents to the correct team, retain the decision trail, and make unresolved exceptions visible to management. The outcome is not merely faster notification. It is a defensible record of control.
Traceability Must Connect Inventory to Conditions
A temperature log proves a room condition. It does not, by itself, prove which inventory was exposed, whether it remained within allowable excursion limits, or whether it was shipped before review. That gap is where many cold-chain investigations become expensive.
Inventory traceability should connect each lot, pallet, serial number, or handling unit to its physical location, movement history, storage requirements, and quality status. In a multi-client 3PL environment, the system must also preserve customer-specific rules. One client may require FEFO allocation and digital proof of outbound temperature, while another may operate under different retention periods or release authority.
When an excursion occurs, the operations team should be able to identify the affected zone and time window, isolate potentially impacted stock, notify the relevant stakeholders, and document the final decision. This includes stock that moved through the affected area, not only stock sitting there when the alarm was acknowledged.
The depth of traceability depends on the product risk. For high-value biologics, batch-level records and tightly controlled disposition workflows may be non-negotiable. For frozen retail products, the approach may focus on pallet-level tracking, storage duration, and evidence of maintained frozen conditions. Both models require a system that reflects real floor movements rather than assumptions made after the fact.
Design for Audits During Normal Operations
The best audit preparation does not begin two weeks before an external visit. It happens every day through disciplined records, controlled access, and exception closure. Auditors typically want to see whether documented procedures match actual practice, whether records are complete and attributable, and whether the organization learns from deviations.
An audit-ready operation can produce calibration records, temperature histories, alarm response logs, maintenance actions, training records, sanitation evidence, inventory holds, release approvals, and shipment documentation without assembling disconnected spreadsheets. Each record should show who performed the action, when it occurred, what changed, and who approved it where approval was required.
Role-based access is particularly important. Warehouse users should not be able to alter quality disposition decisions. Supervisors may need authority to acknowledge an alarm but not to delete the underlying event. Administrators may configure thresholds, but changes should be logged and reviewed. These controls protect record integrity while giving each team the tools they need on the floor.
Electronic systems should also be designed for real operating conditions. Cold rooms affect device batteries. Wi-Fi coverage can weaken around racking and insulated panels. Gloves make detailed touchscreen entry difficult. Offline-capable mobile workflows, barcode scanning, simplified exception forms, and clear task prompts often matter more than an elaborate dashboard.
A Practical Implementation Sequence
Cold storage compliance improvements should be staged around operational risk, not launched as a large technology project with no floor adoption plan. Start by mapping the current product flow and identifying the points where a missed action could compromise product quality, customer commitments, or audit evidence.
Then establish a controlled baseline. Verify sensor coverage and calibration, define storage zones and product rules, standardize alarm thresholds, and clean up location and inventory master data. If product codes do not reliably identify required temperature range, expiry logic, or lot controls, automation will simply reproduce inconsistent decisions faster.
Next, digitize the highest-risk workflows: receiving inspection, temperature excursion management, quality holds, release approvals, and dispatch verification. These are the moments where paper forms, email chains, and verbal handoffs most often leave gaps. Integrate the selected workflows with the existing ERP, WMS, or accounting environment so that inventory status and operational decisions remain aligned.
Finally, measure execution. Review alarm response times, unresolved exceptions, sensor downtime, inventory on hold, expiry losses, out-of-range events, and audit retrieval time. These measures show whether the program is reducing exposure or merely generating more data.
Compliance Is an Operating Discipline
Cold storage facilities do not fail compliance because teams do not understand that temperature matters. They fail when operational reality moves faster than manual controls. A late receiving truck, a door left open, a sensor communication fault, or an unapproved stock movement can quickly become a traceability problem if systems do not connect the event to the inventory and people involved.
The practical goal is simple: make the compliant action the easiest action to perform on every shift. When temperature monitoring, warehouse rules, exception workflows, and audit trails work together, teams spend less time reconstructing events and more time preventing them.
KEEP READING
Want the version that applies to your operation?
Articles only go so far. Book a no-obligation session and we'll walk your process end to end.
Book a demo →